Complete Guide to Flexible Packaging Certifications: ISO 9001, BRCGS, FDA and What Food Brands Must Know
CHAOZHOU, GUANGDONG, CHINA, September 22, 2026 /EINPresswire.com/ -- Global food brand executives and quality assurance
Press Release Disclaimer: This is a press release distributed through the XPR Media network. It has not been independently verified by our newsroom.

CHAOZHOU, GUANGDONG, CHINA, September 22, 2026 /EINPresswire.com/ — Global food brand executives and quality assurance directors actively prioritize verified international certifications to ensure verified consumer safety and streamline cross-border market entry. Packaging materials that touch consumable foods must satisfy stringent global hygiene standards, verified chemical migration limits, and documented traceability protocols. Sourcing certified food contact flexible packaging directly from an accredited manufacturing facility provides brands with validated regulatory compliance and reliable batch consistency. Guangdong Danqing Printing Co., Ltd. (DQ PACK) manufactures certified flexible pouches and barrier films designed for specialty dairy products, infant nutrition, and gourmet seasonings. These precision-engineered packaging solutions protect product purity and reinforce consumer brand trust across international retail markets.
With manufacturing roots dating back to 1991, technical specialists at DQ PACK structure flexible packaging certification evaluation across five foundational pillars:
ISO 9001:2015 Quality Management: Validate systematic operational workflows, standardized documentation, and complete raw material traceability across all production stages.
BRCGS Packaging Global Standard: Confirm GFSI-recognized cleanroom hygiene controls, hazard analysis, and strict contamination prevention protocols.
FDA IMS and Food Contact Compliance: Verify full adherence to United States FDA standards and European Union framework regulations for direct food contact.
AEO Customs Advanced Certification: Leverage Authorized Economic Operator status to expedite international customs clearance and support scheduled logistics delivery.
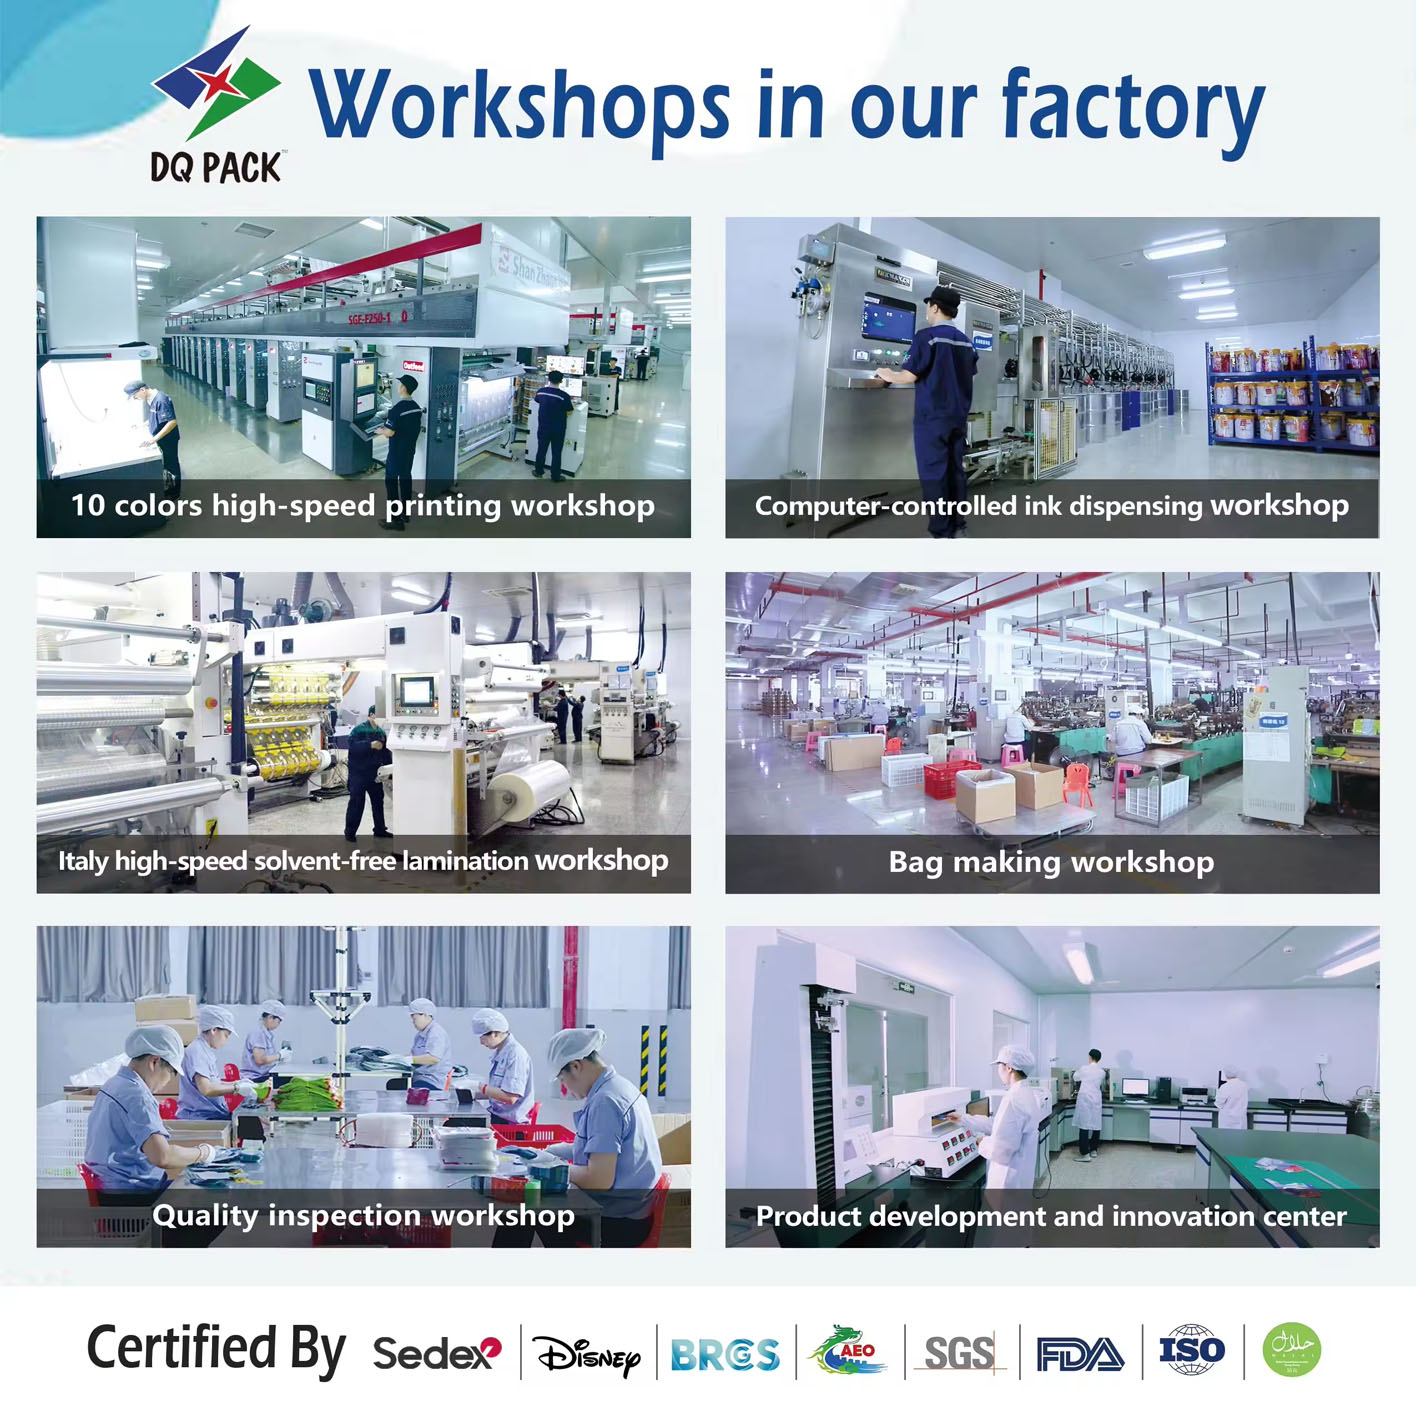
Three-Tier Quality Governance: Audit multi-stage physical testing protocols supported by high-speed LUSTER machine vision inspection across a 35,000 square meter plant.
ISO 9001:2015 Quality Management: Process Standardization and Traceability Systems
ISO 9001:2015 certification establishes the baseline framework for disciplined quality management across modern flexible packaging manufacturing. This standard governs process control across 10 production stages, from design proofing and cylinder engraving to lamination, curing, and carton packaging. DQ PACK maintains computerized batch numbering and enterprise resource planning systems that track every roll of film and batch of adhesive. This digital traceability allows quality teams to verify exact machine operating parameters and operator logs for every production lot. Food brands achieve dependable manufacturing consistency across continuous multi-year supply contracts.
Continuous quality improvement represents a core principle within the ISO 9001:2015 governance structure. DQ PACK conducts regular internal audits, supplier qualification assessments, and statistical process capability studies. Calibrated measuring instruments monitor web tension, drying tunnel temperatures, and cylinder nip pressures in real time. This disciplined operational control ensures exact dimensional accuracy and uniform film thickness across high-volume production orders. Brand owners benefit from reliable packaging performance on automated high-speed filling equipment.
BRCGS Global Standard for Packaging: Cleanroom Hygiene and GFSI Benchmark Governance
The BRCGS Global Standard for Packaging Materials stands as the preeminent benchmark recognized by the Global Food Safety Initiative (GFSI). Achieving BRCGS certification demonstrates an uncompromised commitment to cleanroom hygiene, hazard analysis, and food safety risk management. DQ PACK operates an enclosed Class 300,000 dust-free workshop covering 35,000 square meters, equipped with positive-pressure air filtration and climate control systems. Strict hygiene protocols govern personnel access, gowning procedures, pest control management, and chemical storage throughout the facility. To reinforce environmental compliance alongside hygiene, the plant integrates an advanced Regenerative Thermal Oxidizer (RTO) from Spain’s Tecam Group, ensuring strict VOC emission control under national and international environmental standards.
FDA IMS and EU Food Contact Compliance: Migration Testing and Material Safety
Exporting food products to North American and European markets requires verified compliance with regional food contact material regulations. DQ PACK maintains active FDA IMS (Interstate Milk Shippers) registration and complies fully with United States Title 21 Code of Federal Regulations. All polymer resins, barrier films, and laminating adhesives are formulated exclusively from approved food-contact substances. For European markets, products satisfy European Commission Regulation 10/2011 governing plastic materials intended to come into contact with food. Food processors receive verified Declarations of Compliance backed by certified chemical migration laboratory analyses.
Chemical safety testing verifies that flexible packaging films maintain total inertness when exposed to complex food matrices. DQ PACK tests for overall migration limits and specific migration thresholds using food simulants under extreme thermal conditions. Testing protocols evaluate material behavior during high-temperature retort sterilization at 121 degrees Celsius and long-term ambient storage. The analytical results confirm non-detectable transmission of heavy metals, phthalates, or volatile aromatic amines. This verified material safety preserves the authentic sensory profile and delicate nutritional vitality of packaged infant foods.
AEO Customs Certification: Expedited Global Logistics and Border Clearance
Securing dependable international delivery schedules requires advanced customs accreditation alongside product quality certifications. DQ PACK holds Authorized Economic Operator (AEO) advanced certification issued by international customs authorities. AEO status validates high financial solvency, commercial compliance history, and rigorous physical supply chain security protocols. Export shipments originating from DQ PACK receive priority customs processing and lower physical examination inspection rates. This streamlined customs clearance reduces transit dwell times at major international shipping ports.
Priority trade treatment enables precise coordination of ocean freight, air cargo, and multimodal land transportation networks. DQ PACK maintains dedicated logistics teams that synchronize production completion dates with ocean container vessel departures. Commercial documentation, packing lists, and export declarations are processed through automated digital customs interfaces. Global brand partners in over 140 countries receive reliable delivery timelines for scheduled seasonal product launches. Direct source manufacturing combined with AEO status supports smooth, predictable supply chain execution.
In-House Analytical Laboratories, 3-Stage Inspection, and Global Supply Governance
Maintaining certified quality across high-volume production runs requires advanced laboratory infrastructure and disciplined testing protocols. DQ PACK operates two dedicated testing laboratories spanning 200 square meters, comprising separate raw material and finished product testing facilities. The quality control center is equipped with comprehensive analytical instruments, including gas chromatographs, oxygen permeability testers, and electronic tensile apparatus. Calibrated heat seal testers, coefficient of friction gauges, and cap torque meters evaluate physical integrity across every production batch.
Production quality is further safeguarded by inline LUSTER visual inspection systems operating at speeds up to 300 meters per minute. High-resolution CCD cameras scan the entire printed web in real time, detecting micro-defects including ink splashes and misregistration. Operating within an expansive 35,000 square meter facility housing 60 production machines, DQ PACK maintains BRCGS, FDA, and AEO accreditations. The enterprise delivers verified packaging solutions to over 1,200 commercial clients across more than 140 countries worldwide.
Conclusion
Partnering with a certified flexible packaging manufacturer allows global food brands to ensure verified product safety and accelerate market growth. Founded in 1991, DQ PACK maintains a complete certification portfolio, including ISO 9001:2015, BRCGS, FDA IMS, and AEO accreditations. Supported by a 35,000 square meter facility, 60 advanced machines, and 2 testing laboratories, DQ PACK delivers dependable volume supply. The enterprise provides complete OEM and ODM engineering support to develop customized barrier packaging for multinational food brands. Direct technical collaboration ensures that every package structure delivers verified compliance and superior filling line efficiency. DQ PACK serves as a trusted, accredited manufacturing partner for food and beverage corporations worldwide.
To download official certification credentials, request certified compliance reports, or order free physical test samples, visit the official enterprise portal: https://www.dqpack.com/. For direct quality assurance consultations and commercial wholesale quotations, contact the global compliance and sales division.
GUANGDONG DANQING PRINTING CO.,LTD
GUANGDONG DANQING PRINTING CO.,LTD
+ +86 18125839585
email us here
Visit us on social media:
Facebook
YouTube
Legal Disclaimer:
EIN Presswire provides this news content “as is” without warranty of any kind. We do not accept any responsibility or liability
for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this
article. If you have any complaints or copyright issues related to this article, kindly contact the author above.

Media gallery